If you’ve ever struggled with inconsistent powder flow, air leaks killing your drying process, or frequent breakdowns in your pneumatic conveying line, you’ve probably dealt with rotary airlocks without even knowing it. As someone who’s been in the airlock game for 12 years (working as a supplier, not just a salesperson), I’ve seen folks waste thousands on units that look good on paper but fall flat when the rubber hits the conveyor line. Today, I’m breaking down the real performance indicators that actually matter for these workhorse parts—not just the marketing fluff. Rotary Airlock
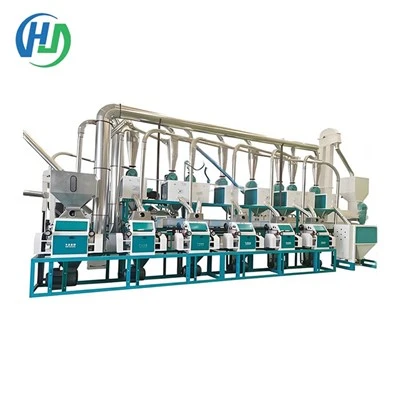
Let’s start with what a rotary airlock even does, just to set a baseline for anyone new: it’s that cylindrical, rotor-filled device tucked between two parts of your process, usually hoppers and conveyors or cyclones and packaging lines. Its whole job is two-fold: move bulk materials (powders, pellets, granules) from one point to another and keep air from leaking through, which would mess up pressure balances, waste energy, or even contaminate products. I’ve seen new operators pick the first airlock they find that fits the size of their pipe, and wonder why their production line is down half the month. That’s because they ignored the key performance metrics that tell you if your airlock is actually working for you.
First up—air leakage rate. This is the big one, and it’s not just a “nice-to-have” number. Air leaks through the gaps between the rotor vanes, the housing, and the end plates of the airlock. If you’ve got a positive pressure side (like a pressure conveying line) and a negative side (like a vacuum conveyor), a leak here will create pressure imbalances that slow your conveying speed by 20-50% in the worst cases. For example, last year I worked with a small food processor making protein powder who was using a cheap, generic airlock. Their leak rate was 15 cubic feet per minute (CFM) at operating pressure, which was dumping so much compressed air into their packaging line that their bag sealer was misfiring constantly. We swapped it for a custom-built unit with precision-machined vanes and end plates, got their leak rate down to 2 CFM, and their downtime dropped by 60% that quarter.
The thing about air leakage is that it’s not one-size-fits-all. What’s an acceptable rate depends on your application: vacuum conveying (most common for lightweight powders) can handle up to 5 CFM per inch of rotor diameter, while positive pressure processes (like moving plastic pellets to an injection molder) need under 1 CFM per inch. Always ask your supplier for the actual tested leak rate at your specific operating pressure, not a generic “under 10 CFM” number. And remember, leakage goes up as your airlock wears—so I always tell customers to check this every 6 months, not just on installation.
Next, volumetric efficiency. That’s how much material your airlock actually moves compared to its maximum rated volume. Let’s say you have a 10-liter airlock—its “rated volume” is how much space is in each rotor pocket. But if your powder is super fine or sticky (think flour, cocoa, or pharmaceutical excipients), it might leave residue in the pockets, so you only get 7-8 liters of material per revolution. That’s a volumetric efficiency of 70-80%. If your product is free-flowing plastic pellets or plastic beads, you might hit 90% or more. Low volumetric efficiency isn’t a death sentence, but if you’re sizing your line to move 500 kg/hour, and your airlock is only hitting 70% efficiency, you’ll either have to run it 30% faster (which will wear it out sooner) or buy a larger unit that wastes money upfront.
I’ve seen this mistake a ton: a farm supply company bought a big airlock for their corn grain pellets, thinking more volume = better. But their pellets were slightly damp, so they were leaving 25% of the material in the pockets. They ended up overproducing their line because they had to run the airlock at 20% higher RPM, which caused excessive dust and even damaged their motor. We adjusted their airlock’s rotor pocket angle a little (a small custom tweak) and got their volumetric efficiency up to 88%, so they could run at the original RPM and hit their production targets without extra stress.
Third on the list—rotational speed consistency. Airlock RPM doesn’t just control how much material you move; it has to stay steady even when your feed rate fluctuates. If your airlock speeds up and slows down randomly, your material flow will be inconsistent. For example, if you’re feeding a batch mixer for candy, inconsistent powder flow will throw off the ingredient ratios—bad for quality, and worse if you’re making something for kids. Most good airlocks come with a variable frequency drive (VFD) these days, but I always warn customers to make sure the VFD has speed feedback, not just a manual dial. Cheap units skip this, so they speed up when the line gets backed up, leading to overfeeding and material spillage.
Last year, I worked with a pet food manufacturer whose airlock would speed up every time their hopper ran low, leading to lumpy kibble batches (too much grain in some, too little in others). We upgraded their airlock to a model with a closed-loop VFD, which uses load cells on the hopper to adjust RPM automatically, keeping the feed rate within ±2% of the target. Their batch rejection rate dropped from 8% to less than 1%—that’s tens of thousands of dollars saved a year, just from a small upgrade in speed control.
Then there’s wear rate, which is something most customers don’t think about until it’s too late. Airlocks that move abrasive materials (like sand, metal powders, or cement) will wear down faster, and that wear changes all the other performance metrics I mentioned: gaps get bigger, so leakage goes up; rotor pockets get shallower, so volumetric efficiency drops. What’s a good wear rate? For abrasive materials, a quality airlock should last 1-2 years of continuous operation before you need to replace the vanes or housing. For non-abrasive powders (like sugar, flour), it can last 5-10 years. But cheap, uncoated airlocks might wear out in 3 months when handling abrasive stuff.
I had a construction materials customer who was using a $500 generic airlock for silica sand. It wore out in 4 months, and every time it failed, it caused 2 hours of downtime to take it apart and replace parts. We sold them a unit with hardened chrome vanes and a coated housing, which cost $2,500 upfront, but it’s still running strong 3 years later. When you do the math: 6 replacements a year at $500 each ($3,000) vs. one $2,500 unit that lasts 3 years, you’re saving money long-term, not to mention avoiding lost production.
Oh, and I can’t forget product integrity—especially if you’re in food, pharma, or cosmetics. Performance here means no cross-contamination, no product degradation, and no leaks that could let moisture or dust ruin your material. For example, if you’re handling specialty pharmaceuticals, even a tiny bit of leftover material in the rotor pockets from the previous batch can mess up a new, sensitive product. That’s why most sanitary airlocks (for food/pharma) have quick-disconnect end plates so you can clean them in minutes, not hours. I worked with a small nutraceutical company that was having to take their airlock apart for deep cleaning every batch, which took 2 hours and cost them 10 production hours a week. We swapped in a sanitary airlock with CIP (clean-in-place) capabilities, and they now do a quick 15-minute flush between batches. That’s 8 extra hours of production a week—huge for a small operation.
Wait, let’s talk about a common myth I hear all the time: “Bigger airlocks are always better.” No way. A 12-inch airlock is overkill for a 6-inch pipe, and it will run inefficiently, wasting energy and wearing out faster. The key here is matching the airlock size to your line’s conveying rate, not just the pipe diameter. I had a chemical processor who installed a 10-inch airlock on a 7-inch conveying line because it was the closest one they had in stock. It ran at half the RPM it was rated for, so most of the rotor pockets were empty—volumetric efficiency was only 55%. They ended up wasting 30% of their compressed air because of the high leakage from running it at low RPM. Swapping to a correctly sized 7-inch airlock fixed that, and their energy bill for the conveying line dropped by 25% a month.
So, when you’re evaluating a rotary airlock, don’t just look at the price tag or the size. Ask for three key numbers: tested air leakage at your operating pressure, volumetric efficiency for your specific material, and expected wear rate for your application. And don’t forget to ask about the extras: VFDs with speed control, sanitary design if you need it, and parts availability—because even the best airlock is useless if you can’t get a replacement vane in a pinch.
At the end of the day, I’ve been doing this long enough to know that most airlock problems aren’t about bad design—they’re about matching the unit to the job, and paying attention to the performance metrics that actually impact your bottom line. Too many people treat an airlock like a throwaway part, but it’s one of the most critical parts of your conveying and processing line. A good airlock can boost your production, cut energy costs, reduce downtime, and even improve product quality. If you’re shopping for a new rotary airlock or looking to upgrade your current one, I can help you find the right fit for your specific application, no generic one-size-fits-all junk. Reach out to work through your needs and get a quote that makes sense for your operation.
Grain Processing Line References:
- Bulk Solids Handling, Vol. 35, No. 4, "Rotary Airlock Performance Metrics and Application Best Practices"
- American Society of Agricultural and Biological Engineers (ASABE), Standard S356.3, "Performance Testing of Rotary Air Lock Valves"
- Powder Handling and Processing, Vol. 28, No. 2, "Wear Characteristics of Rotary Airlocks for Abrasive Bulk Materials"
- Food and Drug Administration (FDA), Current Good Manufacturing Practices (CGMP) for Dietary Supplements, 21 CFR Part 111, "Sanitary Equipment Design for Pharmaceutical and Food Processing"
Henan Huinong Machinery Co., Ltd.
Henan Huinong Machinery Co., Ltd. is one of the most professional rotary airlock manufacturers and suppliers in China, featured by quality products and low price. Please rest assured to buy discount rotary airlock from our factory. We also accept customized orders.
Address: No. 6, Northeast Corner of the Intersection of Renmin Road and Zhujiang Road, New District, Huaxian County, Henan Province
E-mail: frank.tang@huinongmachinery.com
WebSite: https://www.huinongmachinery.com/
